


- Home
- Stress relief annealing
Core service
Stress relief annealing
Annealing to reduce residual stresses in large weldments, with a controlled cycle and an annealing chart.
What is stress relief annealing
Lower residual stress, more predictable machining
Stress relief annealing is a heat treatment that reduces residual stresses in a metal part without significantly changing its basic microstructure.
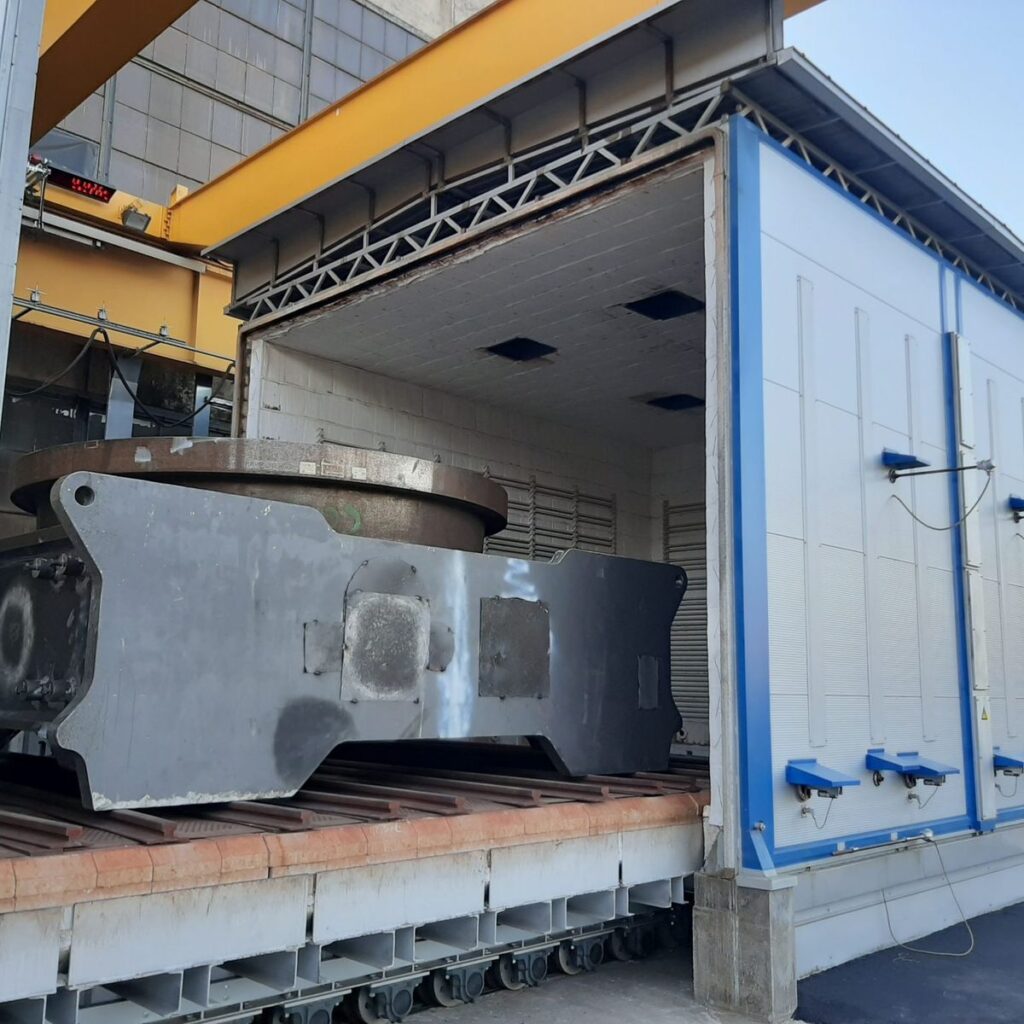
For steel weldments we carry it out after welding (post-weld heat treatment, PWHT), when the effect of stresses caused by uneven heating and shrinkage of the welds needs to be reduced. It is also used for parts after machining and other processes that introduce internal stresses.
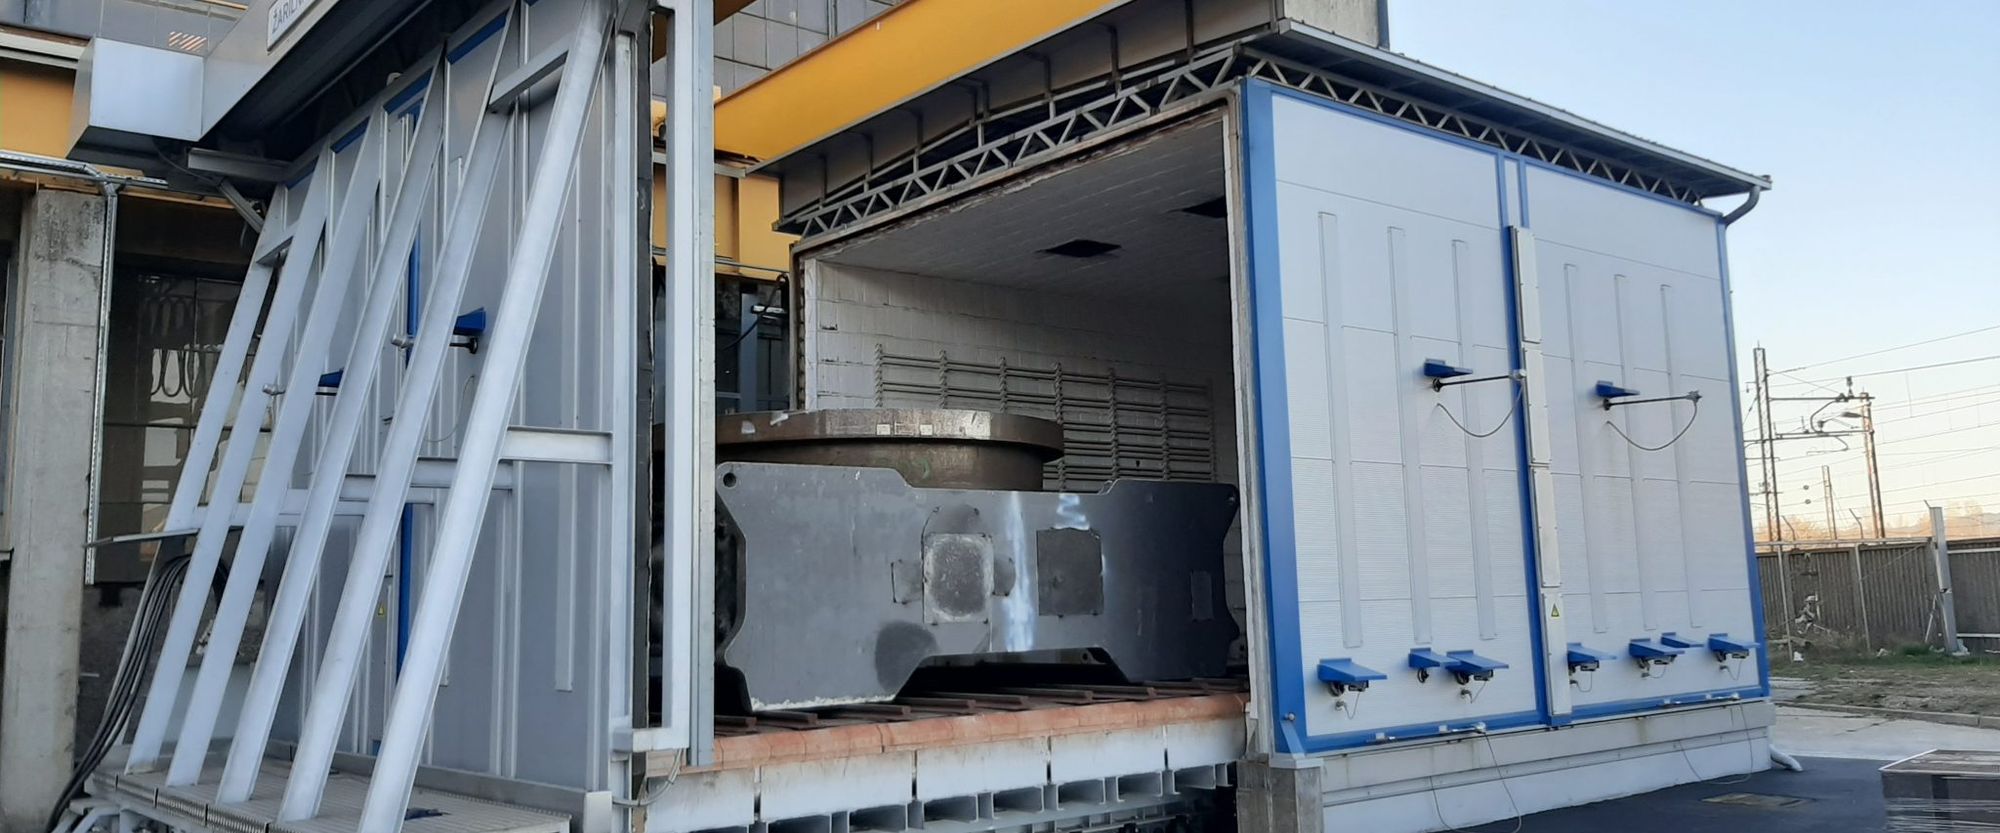
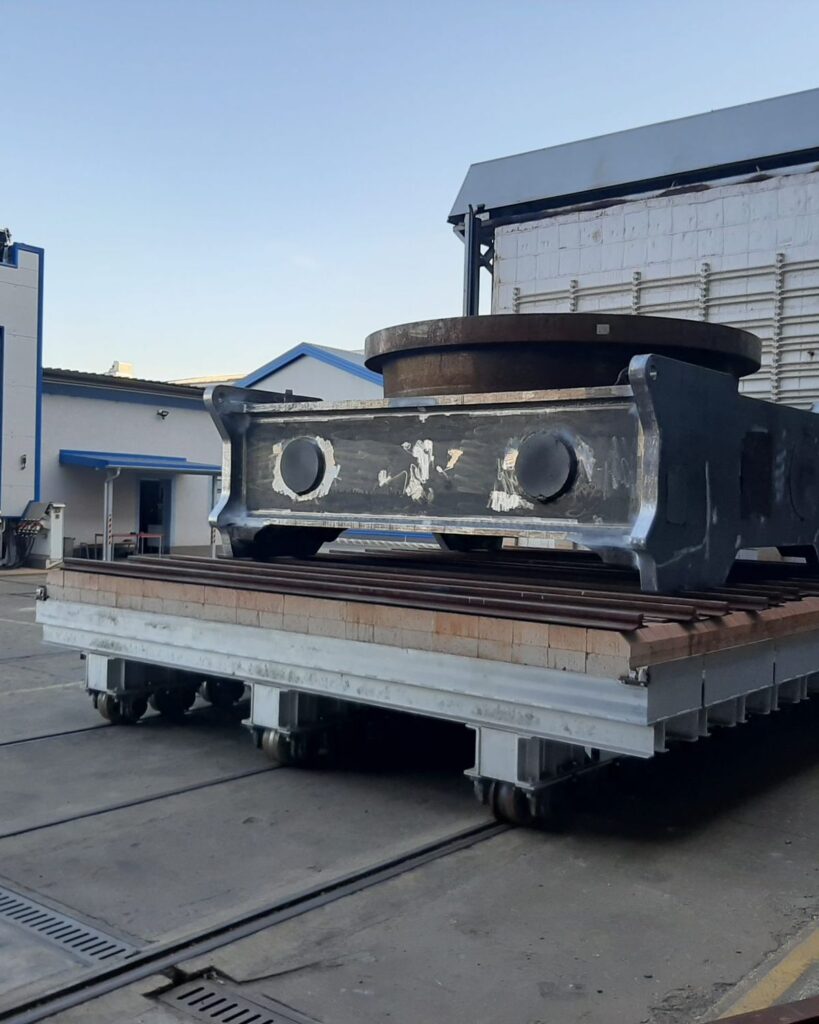
- Weldments up to 12.8 m long and 100 t
- Heat treatment cycle to your specification
- An annealing chart for every cycle
Where stresses come from
Why residual stresses remain in metal
Residual stresses remain in the material even when no external force acts on the part. They are caused by welding, rolling, bending, forging, casting and machining.
Welding
The weld zone heats up strongly and expands, but the cooler surrounding material restrains it. After welding, the weld cools and shrinks, though not at the same rate as the rest of the structure. Part of the stress stays in the part even after it has cooled down.
Machining
A large welded structure is milled after welding. Removing material changes the balance of stresses, parts of the structure may move and the part ends up out of tolerance. Annealing before the critical machining stage reduces this risk.
Objectives
What stress relief annealing achieves
Lower residual stress
A controlled cycle reduces part of the stresses introduced during manufacturing.
Dimensional stability
Lower risk of movement and distortion during further processing.
Ready for precision machining
With tight tolerances, annealing is often an essential step in the production sequence.
Controlled process
Correctly chosen heating, soaking and cooling limit new thermal stresses.
Material properties retained
The aim is to reduce stresses without major unwanted changes to the microstructure or mechanical properties.
Proof of treatment
The annealing chart shows the course of the cycle and can accompany the part documentation.
Process
Stress relief annealing in six steps
Annealing is not just heating a part to a given temperature. Every phase of the cycle matters.
- 1
Preparation and procedure
We check the material, dimensions, weight, geometry and the required cycle, plus any requirements for thermocouples and documentation.
- 2
Loading into the furnace
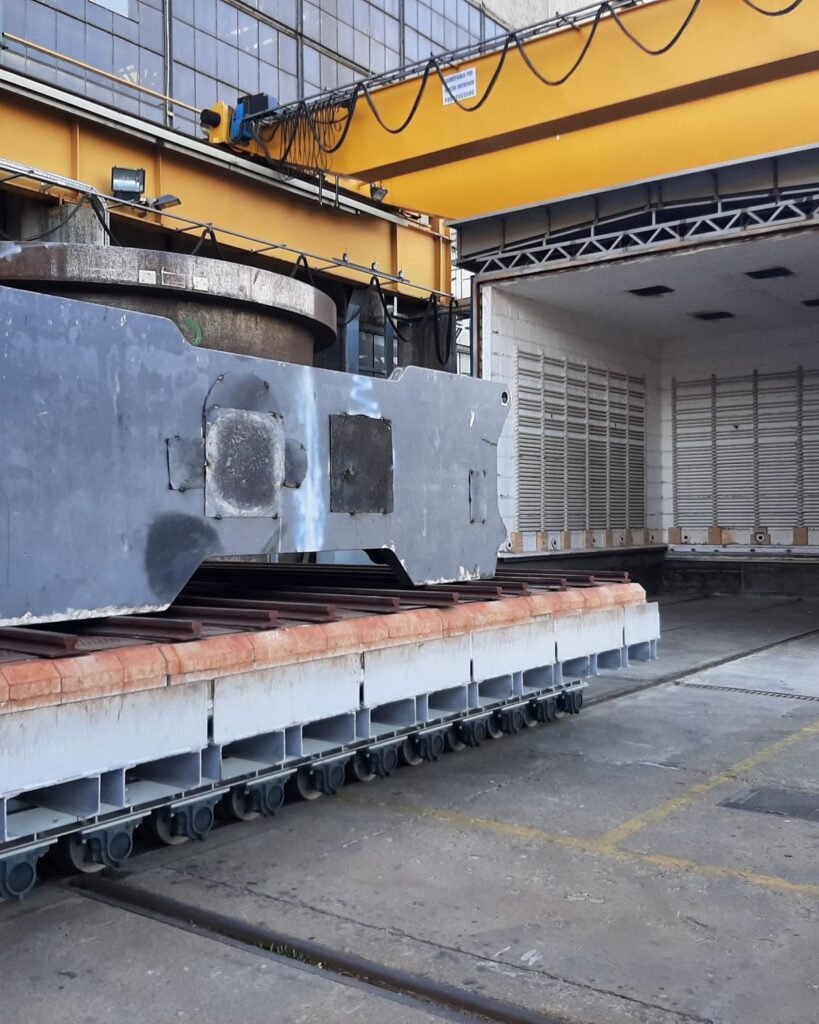
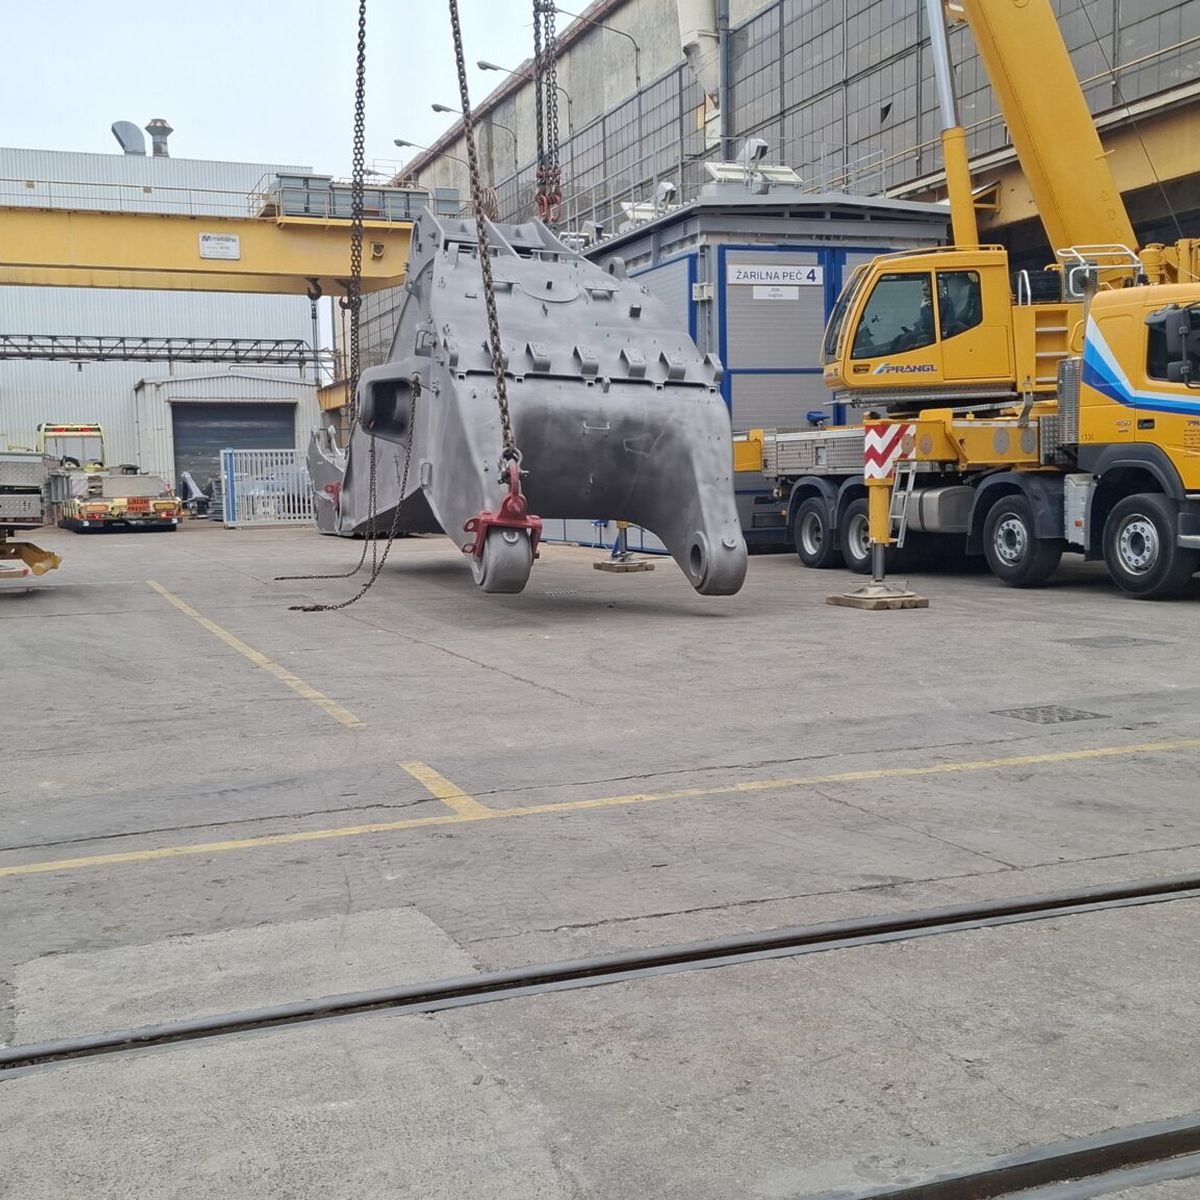
We crane the weldment in and support it according to its weight, shape and thermal expansion. Hollow sections are vented for pressure equalisation.
- 3
Controlled heating
The heating rate is matched to the material and size, as the surface and core of a heavy part heat up at different rates.
- 4
Soaking at temperature
The part is held at the required temperature for as long as the procedure specifies. This is where much of the stress is relieved.
- 5
Controlled cooling
We cool to the specified regime, often together with the furnace, so that no new temperature differences arise.
- 6
Completion and records
We review the temperature record. You receive the annealing chart with the part, plus a report when thermocouples are used.
Heat treatment cycle
Heating, soaking, cooling
For structural steels, technical literature often cites a range of approximately 450–650 °C, but this is not a general rule. The actual temperature depends on the chemical composition, condition of the material, part dimensions and the specified procedure.
With a heavy part it is not enough for the furnace sensor to reach the set temperature. What matters is when the material reaches it. That is why in furnaces 3 and 4 we can measure the temperature directly on the weldment.
Measurement and documentationSuitable parts
What we anneal most often
We check suitability for each part individually, as different steels behave differently when heated.
- large welded structures and heavy weldments
- welded machine components
- structures before precision machining
- parts with complex geometry and tight tolerances
- parts where annealing is specified in the technical documentation
Comparison
Stress relief annealing and other annealing processes
The processes differ in purpose, temperature, soaking time and cooling rate, so they cannot be used interchangeably.
| Annealing process | Main purpose |
|---|---|
| Stress relief annealing | Reducing residual stresses with minimal change to the basic microstructure. |
| Soft annealing | Reducing hardness and improving the machinability of certain steels. |
| Recrystallisation annealing | Removing the effects of strain hardening after cold forming. |
| Normalising | Refining the steel microstructure for a more suitable structure and properties. |
| Diffusion annealing | Reducing chemical inhomogeneity by diffusion at high temperatures. |
Heat treatment regime
What the right cycle depends on
There is no single programme that suits every weldment. Before we start, we take all of the factors below into account.
Material grade
Different steels have different compositions and heat treatment limits.
Wall thickness
Heavy sections heat up and cool down differently from thin-walled ones.
Geometry
Hollow sections and uneven thicknesses affect heat transfer.
Size and weight
A larger thermal mass means a different cycle design.
Customer requirements
Specifications may set temperature, time, rates and measurements.
Further processing
It matters whether the part will be milled, drilled or welded after annealing.
Sequence
Annealing before machining
If annealing is specified or technically advisable, we carry it out before the critical machining stage. A typical sequence is:
- manufacturing the individual parts,
- assembling and welding the structure,
- inspection and preparation of the weldment,
- stress relief annealing,
- further machining,
- final dimensional inspection.
The final sequence is set by the responsible engineer based on the design and requirements of the part.
FAQ
Questions about stress relief annealing
Does stress relief annealing remove all residual stresses?
Does stress relief annealing change the strength of steel?
How long does annealing take?
Can annealing prevent distortion during milling?
Can you anneal very large structures?
Do I receive a temperature chart?
What information should I send with my enquiry?
Enquiry
You send the drawing. We choose the right furnace.
Dimensions, weight and material are enough for us to check which furnace fits and confirm a date.
Send an enquiry